Choosing the China Best Steel Grating Manufacturer for Global Buyers requires more than comparing prices. Steel Grating must support people, equipment, drainage, and daily industrial movement. A strong supplier understands these pressures from real production experience.
This guide examines manufacturers through practical evidence. It considers steel grades, bearing bar dimensions, crossbar spacing, surface treatments, and load requirements. Factory capacity matters, but process control matters more. Look for clear drawings, traceable materials, welding inspections, dimensional checks, and reliable packaging. A serious manufacturer should explain how galvanized grating withstands moisture, handling, and long-distance shipping. Photos help. Inspection records help more.
Communication also reveals expertise. Can the supplier convert a platform sketch into accurate shop drawings? Can engineers recommend serrated surfaces for wet areas? Can they clarify tolerances without hiding behind vague promises? These details separate a dependable partner from a trading contact. References, certifications, test reports, and export experience add authority, but buyers should verify them independently. No brochure replaces evidence.
The lowest quotation may not be the lowest cost. Uneven spacing, weak welds, or poor galvanizing can create installation delays and replacement expenses. Still, no supplier is flawless. Even experienced factories may face material shortages, drawing revisions, or shipment pressure. That reality deserves honest discussion. Global buyers should compare quality, responsiveness, documentation, and after-sales support together. The right China manufacturer is not simply the biggest. It is the one that delivers consistent Steel Grating, explains its limits, and accepts responsibility when plans change.
Choosing a steel grating manufacturer requires more than comparing prices. Buyers must understand the product first. The World Steel Association’s World Steel in Figures 2024 reports 1,892.4 million tonnes of crude steel production in 2023. That scale does not guarantee consistent grating quality. Material certificates, traceability, and dimensional checks still matter.
Steel grating commonly includes welded, press-locked, riveted, and swage-locked types. Welded grating suits platforms and walkways with repeated traffic. Press-locked grating offers a cleaner surface but needs careful load review.
Carbon steel is economical, while stainless steel performs better in corrosive areas. Aluminum reduces weight. Galvanizing should follow ASTM A123/A123M or EN ISO 1461, where applicable. ANSI/NAAMM MBG 531 provides useful guidance for metal bar grating. EN 1991-1-1 defines imposed loads, but it does not replace a product-specific capacity calculation.
Tips: Never select a panel by its name alone. Confirm span, bearing-bar size, spacing, support width, surface finish, and deflection limits. A 1.2-meter trench crossing may face different forces from a maintenance platform. Wheel loads can be especially demanding. Ask for tested load tables and project calculations. One imperfect assumption can cause costly redesign. In practice, many errors begin with unclear drawings, not weak steel.
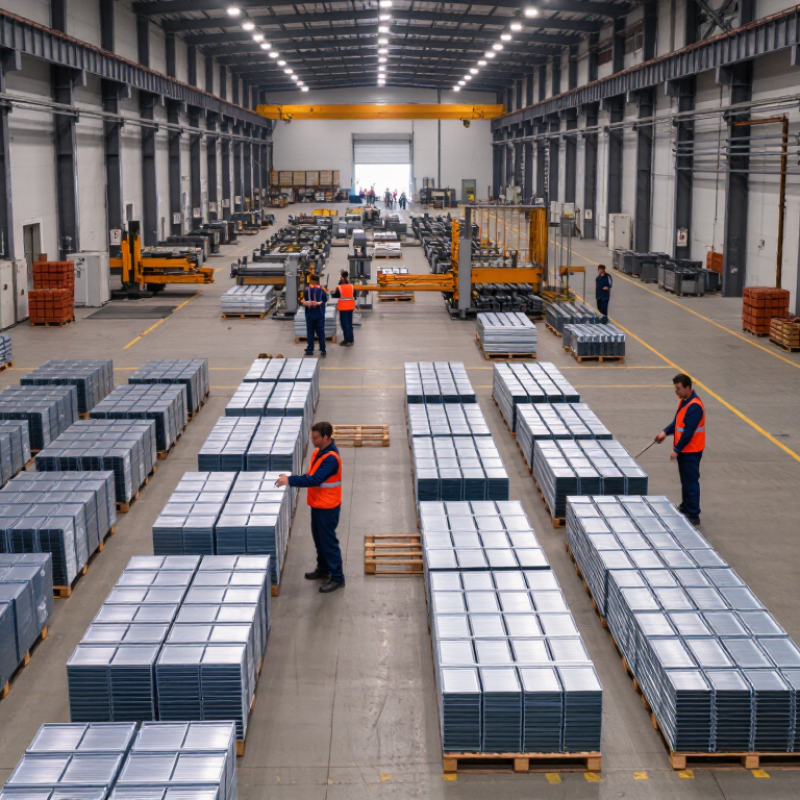
China’s large steel grating production base supports steady supply for overseas construction and industrial projects. Multiple fabrication lines can handle welded, press-locked, and heavy-duty grating orders. This capacity helps buyers manage phased deliveries without restarting production each month.
Practical sourcing experience shows that factory control matters more than volume alone. Reliable producers check bearing bar size, crossbar spacing, weld strength, and panel flatness. Hot-dip galvanizing is inspected for surface coverage and drainage around corners. The details matter. Batch records also connect raw steel certificates with finished panels, making quality discussions more precise.
China’s export network adds another advantage. Manufacturers can prepare custom dimensions, edge bars, stair treads, and cut-outs before container loading. Careful packing reduces movement and coating damage during sea transport. Export teams commonly coordinate drawings, packing lists, inspection files, and destination requirements. This saves time for contractors working across different regions. Yet scale is not perfection. Busy factories may face scheduling pressure, uneven communication, or small dimensional differences between batches. Buyers should approve drawings, sample panels, tolerances, and inspection points before mass production. Clear documents often prevent expensive corrections at the jobsite.
China maintained annual crude steel production above 1 billion tonnes while steel product exports increased strongly, supporting large-scale and globally competitive manufacturing supply chains.
Data sources: World Steel Association, World Steel in Figures 2021–2025; General Administration of Customs of the People’s Republic of China. Crude steel production is shown in million tonnes; steel exports are shown in million tonnes.
China Best Steel Grating Manufacturer for Global Buyers?
For global buyers, steel strength and zinc coating thickness deserve close attention. A stated range of 275–550 MPa can cover different loading requirements. However, strength should not be judged from a brochure alone. Ask for mill certificates, heat numbers, and independent tensile test results. Yield strength and tensile strength are different values. Confusing them can lead to poor specification decisions.
Hot-dip galvanized grating with a 60–100 μm zinc coating offers stronger resistance against moisture and industrial exposure. Coating thickness should be checked on the surface, edges, welds, and cut areas. A magnetic thickness gauge can reveal uneven protection quickly. Look for a documented sampling plan. One reading is not enough. Small uncovered areas may become early corrosion points.
Practical inspection also includes bearing bars, cross bars, weld quality, panel dimensions, and flatness. A 550 MPa material may sound stronger, but it is not automatically the best choice for every walkway. Design loads, span, impact, and installation conditions still matter. I have seen specifications focus heavily on strength while ignoring damaged galvanizing at drilled holes. That is an easy mistake. Buyers should review test records, coating reports, packaging photos, and pre-shipment inspections together. Specifications can still be imperfect. Careful verification reduces the gap between paper quality and site performance.
| Quality Dimension | Typical Specification | Common Verification Method | Reference Standard / Note |
|---|---|---|---|
| Steel strength class | Minimum yield strength: 275–550 MPa | Tensile test on representative steel samples | Actual values depend on the selected steel grade and thickness |
| Q275 structural steel | Yield strength: ≥275 MPa; tensile strength: typically 410–550 MPa | Mill test certificate and laboratory tensile test | Values vary with product thickness and applicable national standard |
| Q355 structural steel | Yield strength: ≥355 MPa; tensile strength: typically 470–630 MPa | Mill test certificate and laboratory tensile test | Often selected for higher-load industrial platforms and walkways |
| Q550 high-strength steel | Yield strength: ≥550 MPa; tensile strength: typically ≥670 MPa | Certified mechanical-property testing | Use only when the structural design and fabrication process are qualified for the grade |
| Bearing bar depth | 25, 30, 32, 40, 45, 50, 60, 65 or 75 mm | Dimensional inspection using calibrated gauges | Selection depends on span, load, support conditions and deflection limits |
| Bearing bar thickness | 3, 4, 5, 6 or 8 mm | Micrometer or vernier-caliper measurement | Nominal thickness should be confirmed on approved drawings |
| Bearing bar spacing | Common center-to-center spacing: 30 or 40 mm | Dimensional inspection against fabrication drawings | Other spacing options are available for access, drainage or load requirements |
| Cross-bar spacing | Common center-to-center spacing: 50, — 100 mm | Visual and dimensional inspection | The selected spacing affects walking comfort, drainage and object passage |
| Hot-dip galvanized coating | Typical project target: 60–100 μm | Magnetic or electromagnetic coating-thickness gauge | Coating thickness depends on steel thickness and the governing galvanizing standard |
| EN ISO 1461 coating benchmark | For steel >6 mm: average ≥85 μm; local minimum ≥70 μm | Coating-thickness measurement at defined inspection locations | For steel 3–6 mm, the standard values are lower: average ≥70 μm and local minimum ≥55 μm |
| Weld quality | Continuous, secure welds without visible cracks, lack of fusion or excessive spatter | Visual inspection; additional non-destructive testing where specified | Welding acceptance criteria should be stated in the purchase specification |
| Load and deflection performance | Project-specific design load and allowable deflection | Engineering calculation or load testing when required | No universal load rating applies; span, bar size, spacing and support conditions must be evaluated together |
Note: Mechanical properties, dimensions and galvanizing requirements should be confirmed against the applicable contract specification, approved drawings and current material standards before production.
Selecting a Chinese steel grating manufacturer requires more than comparing prices. ISO 9001 shows that a documented quality system exists, but it does not guarantee perfect grating. Ask for the certificate scope, issuing body, expiry date, and recent audit records. Then compare those documents with production reality. Are steel coils identified by heat number? Are welding checks recorded? Small details often reveal control.
EN 1090 matters when gratings form part of a load-bearing steel structure. Confirm the manufacturer’s execution class, welding procedures, personnel qualifications, and factory production control. Request traceable inspection files for a similar project. A polished certificate may still hide weak process discipline. Visit the workshop if possible. Check cutting accuracy, weld consistency, and storage conditions.
ASTM A123 applies to hot-dip galvanized iron and steel products. It covers coating requirements, appearance, and testing methods. Ask whether the grating is galvanized after fabrication, not merely painted. Review coating thickness results from representative samples, especially around welds and edges. ISO 9001, EN 1090, and ASTM A123 serve different purposes; one cannot replace another. I would also inspect packaging, because bent bearing bars can appear only after ocean transport. No evaluation is flawless. Supplier documents can be outdated, and factory visits show only one production day. A practical buyer keeps questioning the evidence.
A reliable steel grating purchase starts with measurable tolerances, not attractive samples. Specify bearing bar depth, width, spacing, panel length, and acceptable camber. Ask for inspection records linked to your purchase order. In practice, I have seen small spacing errors complicate installation beside stair stringers.
“Standard tolerance” is too vague. Request the applicable standard and a signed dimensional report. Clarify whether measurements occur before or after galvanizing, because coating can affect final dimensions.
Tips: Send a marked drawing with reference points, load requirements, surface finish, and cutout locations. Verify certificates directly with the issuing organization when possible. ISO 9001 supports process control, but it does not prove every batch meets your design. Material certificates, coating thickness readings, and independent inspection provide stronger evidence. Review the certificate scope carefully.
Packaging deserves equal attention. Use steel frames, separators, lifting points, and moisture protection for long ocean routes. Each bundle should show piece count, weight, drawing number, and destination marks. Photograph loaded containers before sealing.
Lead time should include drawing approval, material preparation, fabrication, galvanizing, inspection, and loading. Add realistic buffer days for port delays. Fast promises can hide missing inspection steps. A checklist reduces risk, but it is not foolproof; revise it after every shipment.

Signup our newsletter to get update information, promotion or insight.